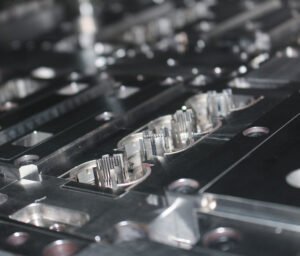
Injection molding gate design starts with the part’s function: choose an entry location, gate type and geometry that can fill the cavity while meeting assembly, strength and appearance requirements. A gate is the opening through which molten plastic enters a cavity; separating the feed material can leave a witness mark on the finished part. [1] Protolabs. The useful engineering question is therefore not simply “where can a gate fit?” It is “which candidate can be manufactured, processed and accepted with evidence?”
Engineering answer in brief
- Mark functional and cosmetic restrictions before comparing gate positions.
- Compare complete flow paths, including obstacles and thickness changes, rather than judging position by distance alone.
- Review predicted weld lines against actual load paths and appearance zones.
- Specify the gate dimensions and the permitted finished vestige separately.
- Approve a gate concept through simulation review and representative mold trials, with traceable acceptance records.
This review sequence applies the location principles documented by Autodesk and the geometry/material tradeoffs illustrated by Protolabs. [2] Autodesk; [1] Protolabs.
Define gate-location requirements before selecting a gate
Autodesk’s location guidance addresses competing objectives: maintain filling and packing paths, avoid load-bearing regions, hide the gate scar, provide an escape route for air, and position weld lines where they do not compromise function or appearance. Its rules also distinguish centralized, symmetrical and end-gated arrangements rather than prescribing a single location for every shape. [2] Autodesk.
The recommended first deliverable is a marked drawing. Ask the product engineer to identify mating faces, sealing tracks, fastener interfaces, flexing features and visible surfaces. Mark prohibited regions explicitly. Record who owns each restriction and whether it is mandatory or negotiable. “Gate on the hidden side” is an incomplete instruction if that side is also an assembly datum.
For each permitted region, write a finished-part requirement: how much projection or recess can the assembly accept, what inspection method will be used, and whether trimming is allowed. Do not replace these requirements with a toolmaker’s general promise of a small mark. A visible gate location, a trimmed projection and a local depression are separate decisions that should be approved separately.
| Drawing input | Recommended question | Decision owner |
|---|---|---|
| Assembly interface | Can a residual mark contact, obstruct or displace the mating component? | Product/assembly engineer |
| Loaded feature | Is the proposed gate or flow-front meeting region part of the service load path? | Responsible structural engineer |
| Visible surface | Which viewing conditions and approved samples define acceptable appearance? | Product/quality team |
| Material recipe | Which exact resin, filler and color package is being reviewed? | Material owner and resin supplier |
| Post-processing | Is manual trimming acceptable, and how will its result be inspected? | Manufacturing/quality team |
| Tool access | Can the selected entry, feed system and removal method fit the proposed tool? | Mold designer |
This worksheet is a proposed engineering review aid, not a standard or a statement that SSP has accepted a particular design.
Compare plastic gate types without treating names as specifications
Protolabs illustrates tab, hot-tip and pin/post gate arrangements in its own molding system. A tab enters at a parting-line edge; a hot tip uses a heated nozzle; its pin/post example involves an ejector-related entry and removal arrangement. Those examples show how location, appearance and removal interact, but their dimensional limits and naming conventions are not universal. [1] Protolabs.
For procurement and design review, ask for a section drawing rather than relying on “pin gate” or “small gate” in a quotation. Confirm whether the proposal is a cold-feed or heated-feed arrangement, where material separates, what remains on the part, and which operation removes it. Require the supplier to explain any term whose physical meaning is ambiguous.
| Candidate concept | Review benefit | Question to resolve | Evidence needed |
|---|---|---|---|
| Edge/tab entry | Allows review of a gate on a permitted edge | Is trimming access compatible with the assembly boundary? | Tool section and finished-edge requirement |
| Heated-tip entry | Allows an interior entry candidate to be evaluated | Is the visible witness region acceptable? | Feed-system proposal and sample acceptance plan |
| Pin/post/tunnel proposal | May provide a different entry or separation arrangement | What exactly does this supplier’s term mean? | Section showing separation, ejection and residual material |
| Multiple entries | Allows comparison of a distributed feed concept | Where do the fronts meet, and how will each entry be controlled? | Filling analysis and trial plan |
The table lists review questions, not a ranking. A candidate should be rejected when a mandatory requirement cannot be met, even if another aspect looks attractive. Keep system-cost comparisons separate from gate-location acceptance; SSP’s existing runner-system articles address the wider hot-versus-cold decision.
Select locations using the complete geometry
Autodesk recommends reviewing thicker entry regions to preserve filling and packing paths, while protecting part function and appearance. It also cautions that long narrow parts can require a different orientation strategy from a symmetric shape. These are design principles to evaluate, not proof that the geometric center is best. [2] Autodesk.
Use the CAD model to prepare at least two defensible candidates when the project allows it. For each, trace the likely route to the farthest required feature. Identify the narrow passages, holes, ribs and turns that make a straight-line sketch incomplete. Record which limitations are geometric and which are assumptions awaiting analysis.
A recommended comparison sheet should hold the resin revision, gate geometry, runner concept and process assumptions constant where practical. If candidate A uses a different material or feed system from candidate B, document that change. Otherwise a favorable plot may be incorrectly attributed to the gate position alone.
For the physical tool review, SSP’s injection mold configurations provide a relevant commercial starting point. The article’s recommendations do not confirm that any particular gate system or tolerance is available for an individual order.
Review meeting flow fronts and air escape together
Autodesk describes weld and meld lines as regions where flow fronts meet. Holes, inserts, multiple gates and thickness-related flow differences can create these meetings; changing injection location or thickness can move them. The documentation warns that a coarse mesh may fail to show every weld line. It does not establish a universal percentage strength loss for every part. [4] Autodesk.
The recommended product review is to overlay predicted meeting locations on the drawing’s loaded and cosmetic zones. Ask whether a proposed line crosses a clip root, boss attachment, seal-supporting area or visible face. These locations are review examples, not automatic failure criteria. The responsible engineer must define the relevant component load case and the evidence required for acceptance.
Likewise, mark the proposed last-to-fill regions and ask the tool designer how trapped air will escape. Autodesk explicitly links location and venting review to air-trap prevention. [2] Autodesk. Avoid resolving a concern with an unsupported instruction to raise pressure or temperature. A design change and a process change should each have an identified purpose, supplier limits and a verification plan.
For polypropylene integral hinges, the resin manufacturer’s guidance requires a consistent flow across the hinge web. [6] INEOS. That special constraint deserves its own validation; see SSP’s living-hinge flow and fatigue study for the part-level test questions instead of assuming that a generic gate comparison proves hinge life.
Separate gate sizing from the accepted gate mark
Celanese’s Celcon acetal guide provides material-specific gate-size guidance and relates gate freeze to the release of second-stage pressure in conventional molding. It also advises avoiding entry in service regions subjected to high stress, bending or impact. Those recommendations apply within its acetal processing context; they should not be copied as universal dimensions for PP, ABS or reinforced nylon. [5] Celanese.
The design recommendation is to list gate width/depth or diameter, land length and feed connection separately from the permitted finished-part witness. Record the source of each starting dimension and the intended method of refinement. A customer’s projection limit is not a substitute for an adequate flow design, and a mold drawing’s gate diameter is not the same as an appearance acceptance limit.
Distinguish a thermally sealing conventional gate from a mechanically closing valve-gate proposal when reviewing the feed concept. Celanese discusses both thermal freeze-off and valve configurations for its material. [5] Celanese. Ask the system supplier which mechanism the proposal uses and how the selected closing or holding strategy will be checked on the actual tool.
A hypothetical enclosure comparison: distance is only a screening metric
Assume a flat rectangular teaching model 120 mm long and 80 mm wide. Ignore walls, bosses, holes, runners and material behavior for this calculation. Compare a point entry at the middle of the left edge with a point entry at the rectangle’s center. Every dimension and entry position is hypothetical.
For the edge midpoint, the farthest corner has coordinate offsets of 120 mm and 40 mm. The straight-line distance is √(120² + 40²) = √16,000 = 126.49 mm. For the center entry, the offsets are 60 mm and 40 mm: √(60² + 40²) = √5,200 = 72.11 mm. The reduction in this geometric distance is (126.49 − 72.11) ÷ 126.49 × 100 = 42.99%.
| Illustrative entry | Farthest-corner offsets | Straight-line distance | What remains unanswered |
|---|---|---|---|
| Left-edge midpoint | 120 mm; 40 mm | 126.49 mm | Actual flow route, gate size and pressure demand |
| Rectangle center | 60 mm; 40 mm | 72.11 mm | Visible mark, feed-system feasibility and functional restrictions |
The 42.99% figure is only a reduction in hypothetical Euclidean distance. It is not a measured reduction in injection pressure, fill time, defects, cost or cycle time.
Suppose the center is also the enclosure’s visible face and a drawing prohibits a gate there. That candidate is unavailable regardless of its shorter distance. Alternatively, suppose the permitted edge requires material to pass through a thin connecting region before reaching the far wall. The simple rectangle calculation does not represent that route. These examples explain why the screening calculation is useful for asking questions but cannot select a production gate by itself.
The recommended next step is to compare the permitted candidates in the complete model and record the reasons a candidate is retained or rejected. Do not disguise an unpermitted center location as a viable option merely to improve a comparison plot.
Validate the selected location before approving production
Autodesk calls Gate Location analysis a preliminary input to a full Fill+Pack analysis. Its tools can exclude prohibited regions and recommend locations using geometry, flow resistance and moldability criteria. [3] Autodesk. A recommendation plot should therefore start the engineering discussion, not end it.
Simulation review record
As a proposed review method, retain the model revision, material file, mesh strategy, gate and feed geometry, and process assumptions. Compare candidate filling patterns with the same acceptance questions. Request the predicted meeting regions, end-of-fill behavior and relevant packing observations. Explain which findings are robust and which depend on uncertain inputs.
Keep the conclusions specific: “candidate B avoids the prohibited face in this model” is a documented geometry finding; “candidate B will never crack” requires evidence that a filling plot does not supply. Assign every open question to a test, measurement or supplier review rather than replacing it with a confidence label.
Mold-trial evidence
The recommended trial plan links each requirement to an observation. Record cavity identity and process settings, retain representative fill-stage samples where appropriate, measure the actual gate witness, inspect appearance under agreed conditions, and assess functional parts against the drawing. If a weld region is part of the service load path, define the relevant component test instead of inferring strength from appearance.
| Review question | Proposed evidence | Acceptance basis |
|---|---|---|
| Does the intended region fill? | Traceable trial parts and documented filling observations | Approved complete-part requirement |
| Is the gate witness acceptable? | Measured projection/recess and controlled appearance inspection | Drawing limits and approved samples |
| Does the assembly fit? | Functional assembly check with production-representative mating parts | Product acceptance method |
| Is a critical meeting region acceptable? | Component testing under the specified load/environment | Responsible engineer’s validation plan |
| Can the result be reproduced? | Recorded material, cavity, tool and process revisions | Project qualification requirements |
After the physical mold concept is agreed, discuss the separate manufacturing stage through SSP’s plastic-part molding services. Provide the acceptance record with the drawing so that a quotation addresses the required evidence as well as the part geometry.
Injection molding gate design release checklist
- Mark permitted and prohibited regions with product-owner approval.
- Name the exact resin and material recipe used for review.
- Retain a section drawing defining the proposed gate, feed connection and separation method.
- Record gate dimensions and finished-part witness limits separately.
- Compare complete flow paths and predicted meeting regions against functional zones.
- Review the planned air-escape locations with the mold designer.
- Document simulation assumptions and all unresolved questions.
- Assign measurements, appearance checks and component tests to the release requirements.
- Retain sample identity and approved tool/process revisions.
- Define when material, gate, tool repair or acceptance changes require re-review.
This checklist is an engineering recommendation, not a substitute for project-specific approval. For context about the company’s two tooling families, see SSP’s stamping and molding overview. Send a marked drawing and acceptance questions when requesting a gate-concept review.
Frequently asked questions
Where should an injection molding gate be located?
Choose among permitted regions by evaluating filling, packing, appearance and functional restrictions. Autodesk’s rules include thick-to-thin paths, symmetry where appropriate, load-bearing areas and weld-line placement. No single location is best for every shape. [2] Autodesk.
Does a smaller gate always make a better part?
A small visible mark is only one acceptance objective. Specify the flow geometry and the finished mark separately. Resin-specific sizing guidance, such as Celanese’s acetal recommendations, must be applied within its material context and checked for the actual tool. [5] Celanese.
Can multiple gates remove weld lines?
Do not assume they will. Autodesk identifies multiple entries as one way separate flow fronts arise, and changing entry positions can move the meeting regions. Evaluate the actual fill pattern and the component’s functional requirements. [4] Autodesk.
Does a Gate Location analysis approve the final design?
No. Autodesk describes it as a preliminary input to full Fill+Pack analysis. Treat its recommendation as a candidate for further review, then check the project requirements with representative trial evidence. [3] Autodesk.
What should a buyer send for gate approval?
The recommended package contains released CAD, the exact resin recipe, marked prohibited regions, loaded/cosmetic zones, gate-witness limits, allowed trimming, and the required inspection or functional test. Include approval responsibilities and change-control rules so the decision can be traced later.
Technical references
- Protolabs: Solving Gating Problems in Injection Molding.
- Autodesk: Design rules of polymer injection locations.
- Autodesk: Gate Location analysis.
- Autodesk: Troubleshooting weld lines and meld lines.
- Celanese: Celcon Acetal Processing Guide, chapter 4, printed pp. 4-6 to 4-7.
- INEOS: Polypropylene Processing Guide, printed p. 5.