Progressive die stamping
Custom metal stamping for OEM production, from strip layout and die build to approved samples and repeat supply. Share your drawing, material, thickness and forecast volume for an engineering review.
Send a 2D drawing, material and expected volume to begin.
Components for production assemblies
Custom progressive tooling and stamped components, with the drawing, approval and production requirements agreed from the start.
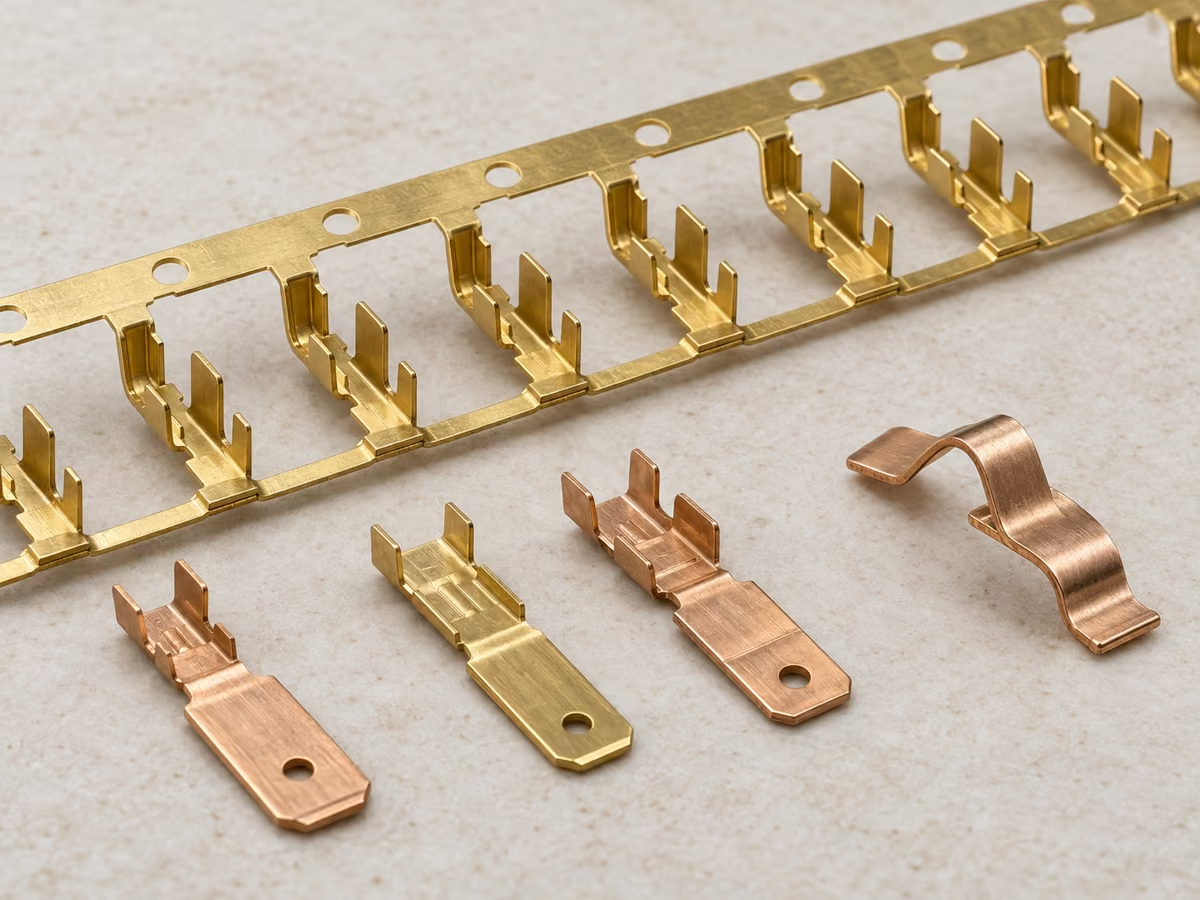
Electrical contacts and terminals
Copper alloy contacts, terminal blanks and carrier strip components for electrical assemblies.
Review conductivity, temper, contact geometry and plating coverage.
Discuss a similar part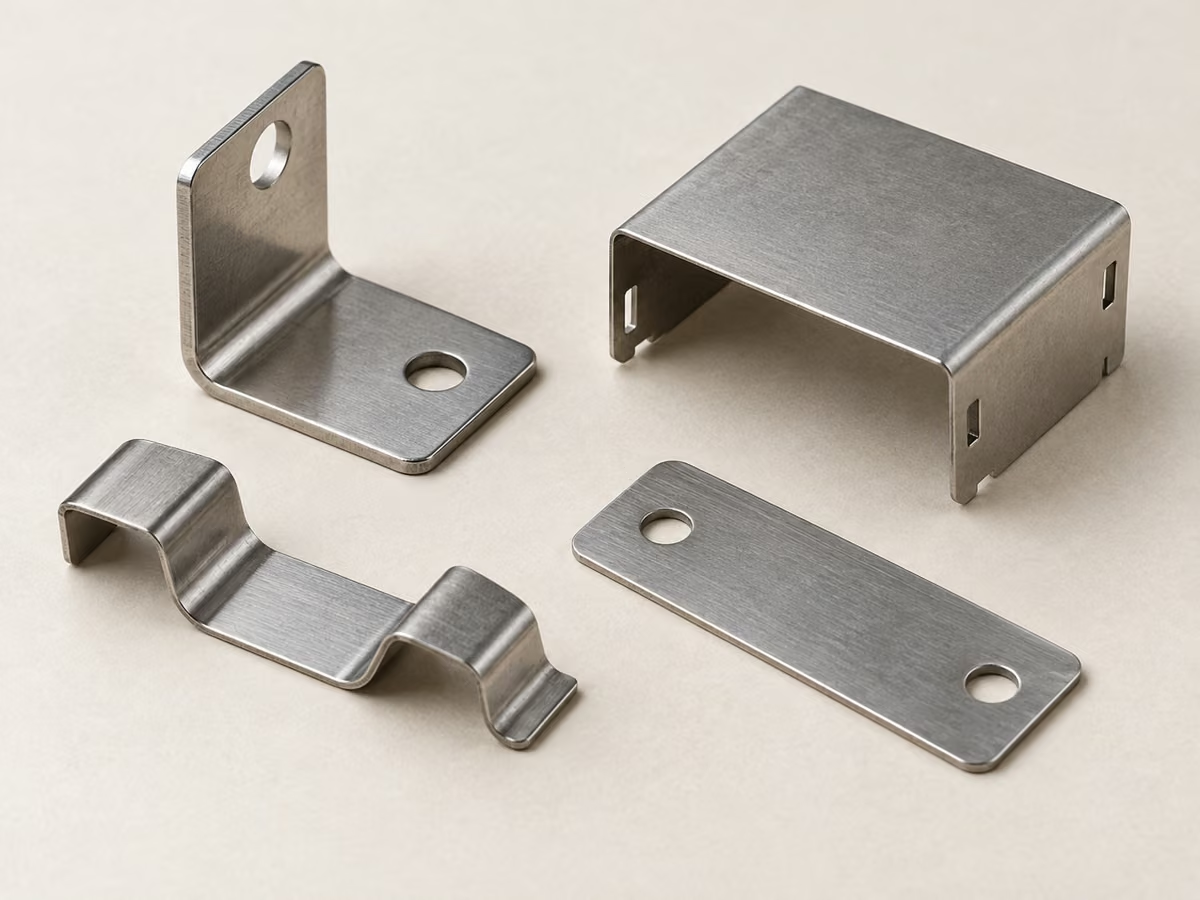
Brackets, shields and retaining clips
Formed sheet metal parts that locate, protect or retain components inside a larger assembly.
Review bend direction, spring function, fastening holes and cosmetic faces.
Discuss a similar part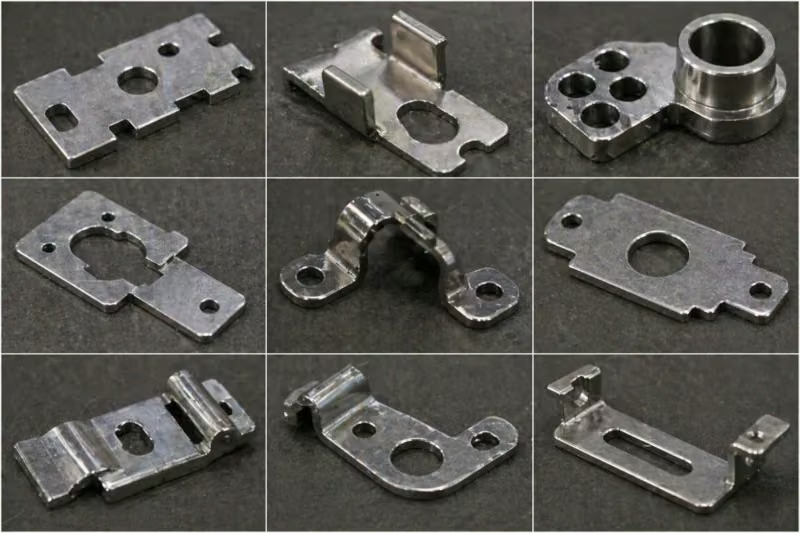
Pierced blanks and formed components
Flat profiles and formed parts with cutouts, slots, mounting holes or local features.
Review hole relationships, edge distance, flatness and burr direction.
Discuss a similar part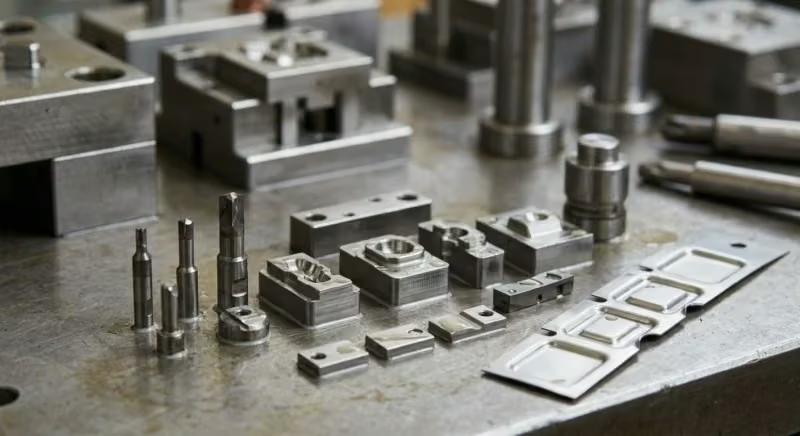
Components retained on strip
Repeated parts carried through the die before separation, or retained on a carrier where the downstream process requires it.
Review strip pitch, part orientation, carrier strength and packing format.
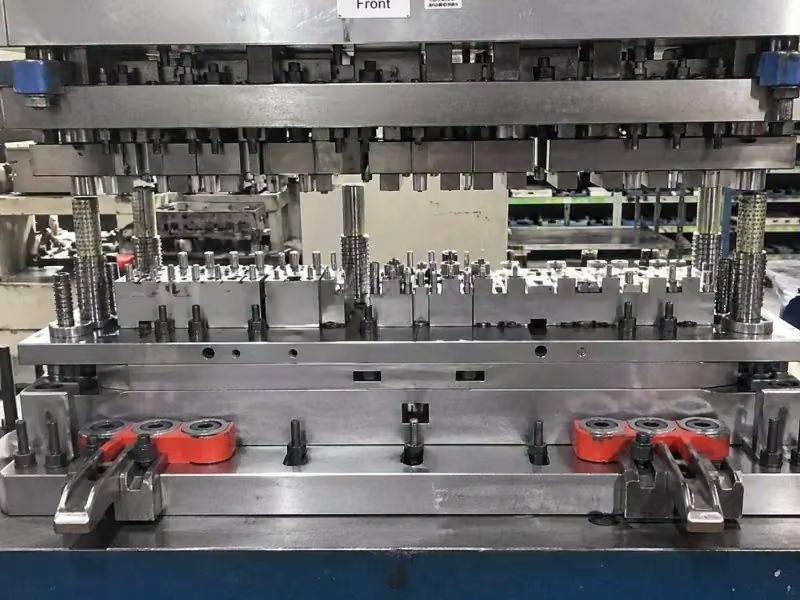
Discuss a similar partIllustrative component examples and tooling photographs. Your part geometry and specifications are confirmed from the drawing.
Stamping services built around your part
A practical route from a controlled drawing to a repeatable production process.
DFM and strip development
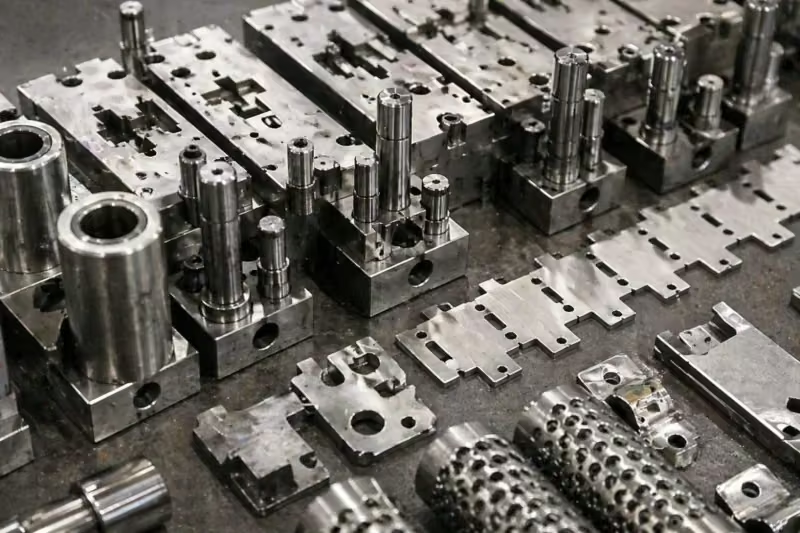
Review bend radii, pierced features, grain direction, carrier stiffness and station sequence. Balance material utilization with reliable feeding and access for inspection.
Progressive die design and build
Develop the die around the agreed strip layout, press interface and maintenance needs. Define punches, inserts, pilots, wear parts and spare component requirements before manufacture.
Tryout and sample approval
Use trial parts to evaluate dimensions, forming behavior, burrs and surface condition. Agree corrections and approval documents before releasing the process for repeat production.
Production, finishing and delivery
Plan stamping, secondary operations and packaging around the purchase order. Confirm the finish specification, inspection records, lot identification and release schedule for your program.
Have a drawing ready?
Share your part requirements to discuss tooling, samples and ongoing supply.
Request a quoteFrom your drawing to a manufacturing plan
Custom geometry, defined materials, agreed quality checks. Tell us what your assembly needs and we will review the route to production.
The right starting point is your component and production plan. We review geometry, material condition, critical features and demand together, then define the tooling, sample approval and supply scope in the quotation.
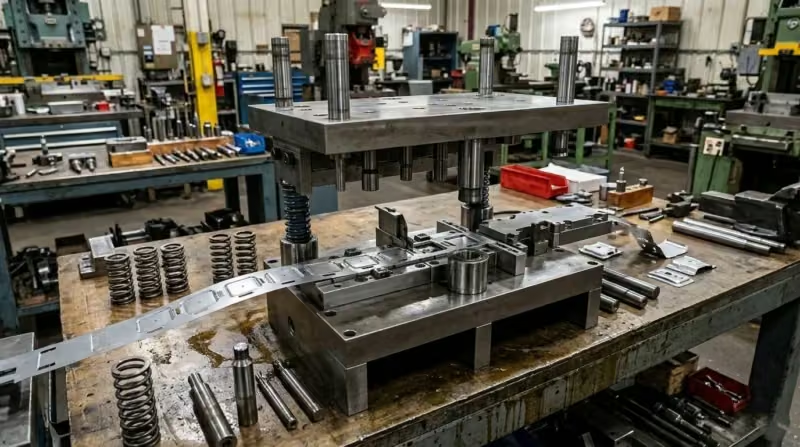
A clear path to production approval
The release points matter as much as the cutting and forming operations. Establish the required evidence at each stage.
Drawing and requirement review
Confirm the drawing revision, material grade, thickness, quantities, datums and critical features.
Output: agreed project inputsStrip layout and die concept
Define feed pitch, carrier, pilot locations, forming sequence and scrap removal. Check the intended press interface.
Output: tooling concept for reviewTool manufacture and assembly
Machine and finish the die components, assemble the tool and check fits, guiding and service access.
Output: assembled die ready for tryoutPress tryout and corrections
Evaluate feed stability, cut edges, springback and part release. Adjust the tool against trial results.
Output: representative sample partsMeasurement and sample approval
Measure agreed features, review material and finish records, and close deviations before release.
Output: approved samples and records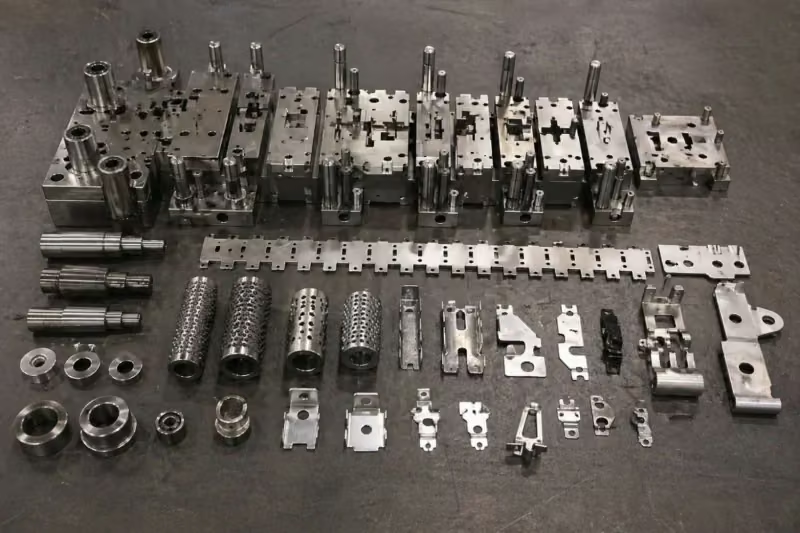
Repeat production and maintenance
Use the agreed inspection plan and lot controls. Schedule maintenance around wear and production needs.
Output: released production lotsDie tooling and stamped component examples.
Quality evidence tied to your drawing
SSP operates under an ISO 9001:2015 quality system. Define the part acceptance criteria and the documentation needed for your supplier approval.
First article measurements
Agree the inspection dimensions, datums, measurement method and report format for representative sample parts.
Production controls
Identify critical features and agree the sampling plan, checks and escalation process. Capability studies apply where specified and validated.
Material and finish records
Define the material certificates, coating evidence and lot references required with the order.
Customer approval documents
Specify PPAP level, control plan, PFMEA or other customer documents in the RFQ so their scope can be confirmed before tooling starts.
Engineer the features that affect assembly
A tooling tolerance is different from a finished part tolerance. Define the functional requirement, then select a practical manufacturing and measurement approach.
Datums and hole relationships
Identify how the part locates in your assembly. Reference holes, slots and formed faces to the datums that matter.
Bends and springback
Review grade, temper, grain direction and bend radius together. Validate final angles and profiles on trial parts.
Cut edges and burr direction
Specify the permitted burr, edge condition and orientation. Tool clearance, wear and deburring all affect the result.
Surface and finish allowance
Identify contact zones and visible faces. Account for coating thickness, masking and handling marks where relevant.
Choose the material and finish as a system
Grade names alone do not define stamping behavior. Include the supply condition, thickness tolerance, finish and operating requirements in the review.
| Material family | Typical purpose | What to confirm |
|---|---|---|
| Carbon and alloy steels | Brackets, formed hardware and general structural parts | Grade, coating, strength, formability and corrosion protection |
| Stainless steels | Corrosion resistant clips, shields and formed components | Grade, temper, grain direction, springback and surface condition |
| Copper, brass and bronze | Electrical contacts, terminals and conductive parts | Conductivity, temper, contact forces and plating requirements |
| Aluminium alloys | Lightweight brackets, covers and thermal components | Alloy, temper, bendability and cosmetic finish |
Secondary operations to specify
Edges and surfaces
Deburring, cleaning and controlled surface preparation according to the part requirement.
Protective and functional finishes
Discuss zinc or nickel plating, stainless passivation, aluminium anodizing or coating where the application calls for it.
Assembly and packing
Confirm any secondary assembly, part orientation, separators and protection for contact or cosmetic surfaces.
Material feasibility, press requirements, achievable tolerances and finishing scope are confirmed against the drawing and quotation. No single tolerance or press speed applies to every stamped part.
Make the tooling investment work for your volume
Progressive tooling can be effective for stable designs and repeat demand. Evaluate the complete program cost rather than comparing piece price alone.
Process fit
Compare a progressive die with simpler tooling for lower quantities or frequent design changes. Consider transfer tooling for geometry that needs independent blanks or different handling.
Tooling ownership and upkeep
Agree ownership, storage, maintenance, spare wear components and the process for engineering changes. Define the delivery scope if the die will run in your press.
Supply and total cost
Review tooling, material use, secondary operations, inspection, packaging and expected ordering pattern together. Confirm capacity and delivery dates during quotation.
Tooling and production support
Explore the manufacturing scope behind your stamped component program.
Progressive die stamping FAQs
When is progressive die stamping a suitable process?
It suits parts that can remain on a carrier strip through successive operations, particularly when a stable design and repeat demand justify a dedicated tool. Geometry, material, batch size and lifetime demand determine the business case; there is no universal minimum volume.
What tolerances can you achieve on my part?
Send the drawing with datums and critical features marked. Thickness variation, material condition, forming geometry, springback and tool wear affect the finished part. The quotation and approved inspection plan establish the tolerances for your application.
Which materials can be reviewed?
Carbon steels, stainless steels, copper alloys and aluminium are common starting points. Share the exact grade, temper, thickness and finish requirements. Other alloys require a feasibility review rather than an assumption that every grade is suitable.
Can you supply the die as well as stamped parts?
We support die engineering and manufacture as well as stamped component projects. Define whether you need a production die, a tool and sample package, or ongoing part supply. For an exported tool, include press specifications and acceptance requirements.
Can you provide PPAP or inspection documents?
Include the required PPAP level, first article report, material certificate, capability study or customer format in your RFQ. Agree the deliverables and validation scope before the tool and production plan are released.
What determines price, order quantity and lead time?
Part complexity, tool size, material, finishing, approval requirements and forecast demand affect cost and scheduling. Tool ownership, sample quantity and production order sizes are quoted for the project. Send your target dates so the plan can be reviewed.
Tell us what you need to make
Start with a drawing and a few project details. Choose the contact route that works for your team.
Project requirements
- 2D drawing and 3D model with revision and critical features
- Material grade, temper, thickness and surface finish
- Annual demand, batch size and target sample date
- Inspection, PPAP, packaging and press details if applicable