Motor lamination stamping burr control needs two separate checks: inspect the cut edges against the lamination drawing, then verify the assembled stack against its own geometry and electrical requirements. A burr can create an unintended conductive contact between layers, but burr height alone does not establish whether a particular stack has an electrical fault. Published experiments on laminated magnetic cores demonstrate the contact mechanism under their own conditions. [3] Hamzehbahmani et al., experimental study. This application study shows how to turn that distinction into an inspection and release plan.
Define the lamination and acceptance criteria
Assume an OEM is evaluating a stamped stator lamination made from coated non-grain-oriented electrical steel with a nominal sheet thickness of 0.35 mm. The example stack contains 200 laminations. Those are planning assumptions, not a recommendation for motor performance or an available SSP grade. For a real trial, the motor engineer must define the specified grade, coating, joining route and stack drawing before the die and inspection plan are approved. Electrical steel suppliers offer insulation and bonding coating systems with different functions; use the documentation for the exact material ordered. [5] voestalpine, electrical industry.
Keep three specifications separate in the purchase and inspection records: the incoming sheet or slit strip, the finished stamped lamination and the assembled core. Incoming stock records may cover grade, thickness and coating. The stamped part drawing identifies controlled cut edges, orientation and burr limits. The assembly drawing identifies stack geometry, the measurement state and any functional tests. Write the stage next to each requirement so the team does not apply a stock acceptance value to a finished slot or a stack dimension to a loose part.
IEC 60404-9:2018 covers methods for geometrical characteristics of electrical steel strip and sheet, including burr height. Its public description characterizes burr height by a maximum and identifies the material scope. [1] IEC 60404-9:2018. That is a useful reference when specifying stock inspection. The public description does not establish a universal burr limit or a complete test procedure for an assembled motor core. Agree the finished-part acceptance method on the drawing or in the inspection plan and confirm whether a specific standard is contractually applicable.
Why an edge burr matters in a motor stack
A lamination burr is a projection at a cut edge. In the cited experimental work, the researchers compared cuts made with sharp and blunt guillotines and showed an example of edge burr contact between stacked layers. The specimen was 0.30 mm grain-oriented electrical steel, cut by guillotine, with four layers in the illustrated stack. [3] Hamzehbahmani et al., experimental study. That evidence supports the mechanism. It does not provide a transferable stamped-stator limit for the hypothetical coated 0.35 mm sheet.
If contacting edges form an unintended electrical path, the result depends on the path and the magnetic conditions. Published equivalent-network work examines interlaminar faults and loss across flux and frequency conditions. [4] Hamzehbahmani et al., electrical-network study. For the trial, use an observed high burr as a reason to inspect the specified edge and assembled stack. Do not convert a height in micrometres into watts of loss. Even a dimensional pass cannot substitute for electrical acceptance where the OEM requires it.
Cutting edge condition, clearance and sheet characteristics can influence the resulting burr. [3] Hamzehbahmani et al., experimental study. Use them as diagnostic leads rather than automatic corrections. A repeated peak at one slot is an instruction to preserve the feature and tool position in the record. A change after stock replacement is a reason to compare both stock and die history. If punch offset is suspected, use the separate one-sided burr diagnostic study to investigate alignment. Here, the decision is whether the lamination and the resulting stack have enough evidence for release.
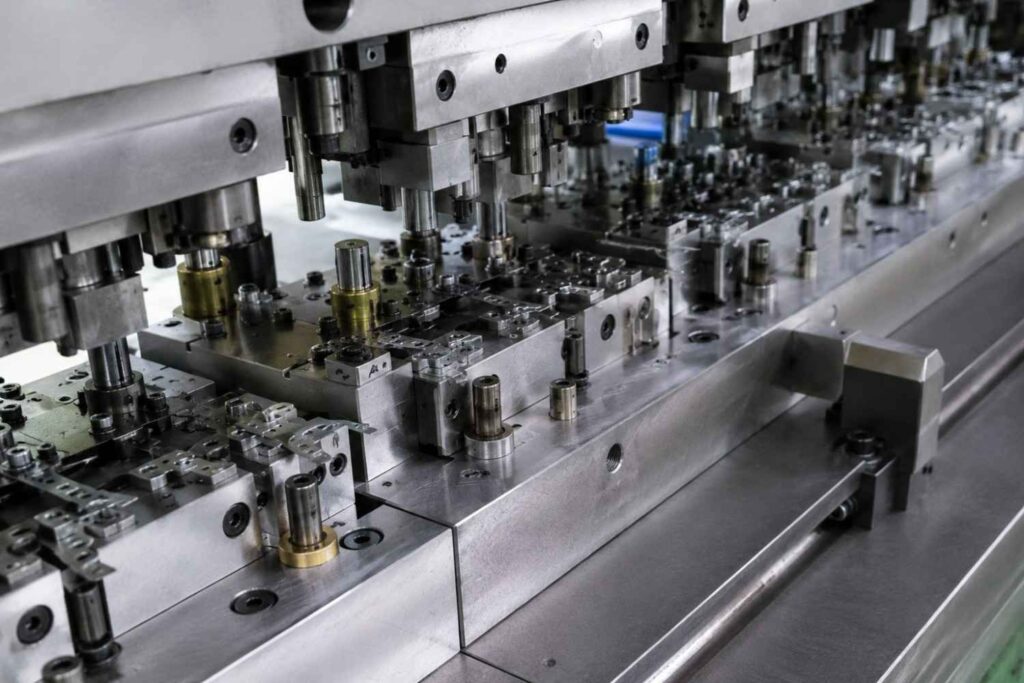
How to inspect burr height on stamped motor laminations
Map the edge before taking a reading
Give each trial part an identifier and mark the reference orientation on a drawing or image without changing the measured edge. In this proposed plan, the outer profile, bore, slot opening and slot root are separate inspection regions. Record the cut face, clock location and tooling station where known. Specify how far each region will be scanned and which areas are inaccessible. A reading from an easy outer edge cannot be used as a proxy for a slot root that the instrument did not reach.
Define the reference surface and the direction of measurement before comparing numbers. For this example the quantity is the greatest observed projection normal to a defined adjacent sheet face within the mapped region. Select a method that resolves that feature on the real geometry; check access, part support, calibration and repeated readings around the same location. In particular, agree how the local plane will be established and how tilted parts, curved edges or surface debris will be handled. A result taken after brushing an edge belongs in a different inspection state from an as-stamped result.
Make the decision rule explicit
Assume the OEM sets a maximum of 25 µm, equal to 0.025 mm, on the mapped finished edges. Assume an illustrative expanded uncertainty of 3 µm for the chosen method. Neither number is a published specification or a claimed instrument capability. Use this example rule only: accept an individual result if reading plus uncertainty is at or below 25 µm; reject it if reading minus uncertainty exceeds 25 µm; otherwise hold it for disposition. An actual quality plan must define its own decision rule, how the uncertainty was established and who can authorize a disposition.
| Mapped region | Observed maximum (µm) | Reading ± 3 µm | Example disposition |
|---|---|---|---|
| Outer profile | 16 | 13–19 | Accept region |
| Bore sector | 19 | 16–22 | Accept region |
| Slot opening | 24 | 21–27 | Hold: interval crosses limit |
| Slot root | 29 | 26–32 | Reject region: lower bound exceeds limit |
The average of the four readings is 22 µm, below the assumed limit. That average does not change the disposition of the slot root because the drawing in this example limits the maximum at each controlled region. Under the assumed rule the lamination fails. Keep the peak record and the part ID, and investigate the hold result separately. Neither an average nor the use of additional decimal places can turn an unresolved measurement into a pass.
For a real trial, retain parts from defined time points, including after setup or a tool intervention and during the agreed production window. Preserve lot, station and tool revision alongside the results. The quality engineer should set sample size and frequency from the risk and expected variation; the four regions above are not a sampling plan. If a method cannot see a critical edge, qualify a different inspection approach or keep that region open in the approval record.
Check motor lamination stack quality separately
Separate height from material stacking factor
Define how stack height will be measured: the joining condition, count, axial locations, fixture, load or restraint state and timing relative to assembly. Record local heights where the drawing requires them, because a single reported value may not describe the assembly conditions of interest. Keep the unit, fixture revision and part count with each result. If the joined and loose states are both inspected, report them separately.
For a simple planning comparison, let N be the layer count, t the nominal sheet thickness in millimetres and H the assumed stack height in millimetres. N × t = 200 × 0.35 = 70.00 mm. Define a nominal thickness ratio as 100 × N × t ÷ H. For H = 72.00 mm this gives 97.22%. This is bookkeeping based on nominal input, with no correction for coating or other contributions. It does not determine steel volume fraction, material stacking factor, electrical isolation, or how much of the 2.00 mm difference comes from a burr.
| Assumed stack height H (mm) | H − N × t (mm) | Nominal thickness ratio |
|---|---|---|
| 71.80 | 1.80 | 97.49% |
| 72.00 | 2.00 | 97.22% |
| 72.40 | 2.40 | 96.69% |
IEC 60404-13:2018 describes methods to determine stacking factor of electrical steel strip and sheet, along with resistivity and density. [2] IEC 60404-13:2018. Report a supplier’s standard-based material result with its stated method and material scope. Keep that result in a different field from the nominal thickness ratio and the finished assembly height. For example, comparing the 97.22% arithmetic value directly against a material datasheet limit would conflate different quantities.
If the stack is outside its drawing limits, compare verified count, incoming sheet data, measured lamination condition, joining method and fixture state before assigning a cause. If the assembled core is within its height limits but electrical acceptance is open, keep the functional gate open. The electrical or motor engineer should select the applicable test and conditions based on the design rather than treating a geometric check as a magnetic or insulation qualification.
Decide whether the trial can be released
In the example, the slot-root result blocks release even if the assumed height is acceptable. A corrected trial should retain the original and corrected samples, record the authorized change, repeat the affected dimensional checks and include a stack made from traceable parts under the approved assembly conditions. If the proposed correction involves deburring, verify the resulting edge geometry and coating condition. The experimental literature discusses the possible effects of deburring on dimensional accuracy, surfaces and stresses. [3] Hamzehbahmani et al., experimental study.
| Gate | Evidence to retain | Action if incomplete |
|---|---|---|
| Incoming material | Grade, nominal thickness, coating, stock lot and applicable supplier results | Separate unverified lots and confirm specification |
| Stamped lamination | Edge map, maximum readings, method, uncertainty and affected-part traceability | Hold or reject per the agreed rule; document corrective trial |
| Assembled core | Count, joining and restraint state, height locations, drawing checks | Resolve assembly discrepancy before approval |
| Functional validation | Design owner’s specified test, conditions and recorded acceptance | Keep functional sign-off open until valid evidence exists |
For a tooling enquiry, share the lamination and stack drawings, grade and coating, critical cut-edge map, agreed inspection method and the applicable acceptance gates with SSP Precision. The stamping die portfolio provides tooling configuration context; the die manufacturing service describes drawing review and press tryout. Ask how the proposed tool trial will produce evidence for the named requirements before committing to the route.
Frequently asked questions
Is 25 µm a standard lamination burr limit?
No. It is a hypothetical drawing limit chosen to demonstrate the decision rule. Confirm the finished-part specification with the motor design owner; a strip test method or stock limit cannot be assumed to apply to every stamped feature.
Does a burr within tolerance prove electrical isolation?
No. The geometric reading supports the edge requirement only. Conductive paths and electrical effects depend on the assembled condition and excitation. Use the specified functional acceptance method where required. [4] Hamzehbahmani et al., electrical-network study.
Can a good average override a high burr at one slot?
No, if the drawing controls the local maximum. Apply the decision rule to the observed peak at the specified region and retain its location and part identifier.
Is the nominal thickness ratio the IEC stacking factor?
No. The example divides a nominal thickness sum by an assumed assembled height. It is not a measurement under IEC 60404-13. [2] IEC 60404-13:2018.
Technical references
Reviewed 6 November 2026. The IEC references are public scope descriptions. Published studies explain mechanisms under their test conditions; the application worksheet and all trial entries here are illustrative.