

Custom Tooling Spare Parts Manufacturing Made to Your Print
Tooling spare parts manufacturing for precision punches, die inserts, guide components and mold core inserts. SSP makes replacement parts from approved drawings or samples, with machining, grinding and inspection planned around the critical fits in your tool.
Send STEP, IGES, DWG, DXF or PDF files. An engineer replies within 24 hours, Mon–Fri, 9:00–17:00 China Standard Time.
An Extension of Your Toolroom for Made-to-Print Tooling Components
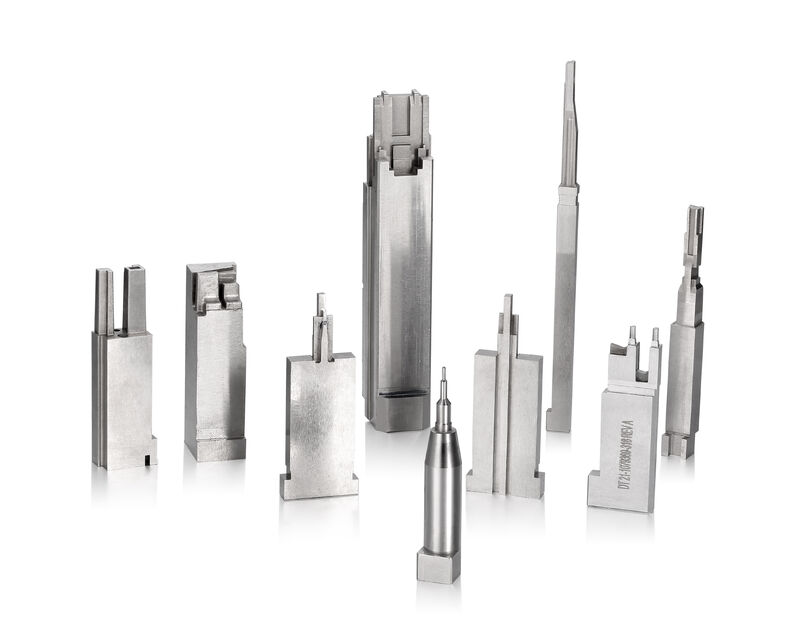
SSP has built progressive dies, injection molds and their replacement parts in Humen, Dongguan since 2008. Our tooling fabrication team reviews how custom tooling components locate, slide and wear inside the assembly. Component machining is planned around drawing datums, material, heat treatment and the features that control interchangeability.
Order custom tooling spare parts manufactured to your drawings, from a single replacement to repeat batches. Send the drawing revision, quantity, material, hardness and coating, and identify worn mating surfaces that may affect fit. For catalog dimensions, see our tooling spare parts catalog.
- Stamping plants
- Mold shops
- OEM maintenance teams
- Tooling distributors
Made to print, or from your worn part
Send 2D or 3D files, or ship us the worn component. We measure it, draw it and send the drawing for your approval before any steel is cut.
Engineering review on every RFQ
Each quote comes with DFM notes on tolerances, grind stock, material and heat treatment, so problems are solved before machining starts.
Certified, documented quality
ISO 9001:2015 and IATF 16949 certified quality system. A dimensional report, material certificate and hardness results ship with every order; FAI and PPAP documents on request.
One spare or a production batch
No minimum order. We keep your drawing revision on file, so repeat orders ship as exact, interchangeable replacements.
Tooling Spare Parts Manufacturing: 7-Step Order Process
One project engineer owns your order from drawing review to dispatch. You get a quote with DFM notes within 24 hours, a confirmed ship date, and inspection data before the parts leave Dongguan.
- A single contact who speaks with your toolroom in engineering terms
- Progress updates at material, heat treatment and final inspection
- Drawing revisions controlled, so repeat orders match the last batch
RFQ & drawing review
2D/3D files or a worn sample. Quote with DFM notes within 24 hours.
DFM & process plan
Clearances, datums and grind stock agreed with you before cutting.
Certified material
Tool steel, carbide or mold steel, with mill certificates on file.
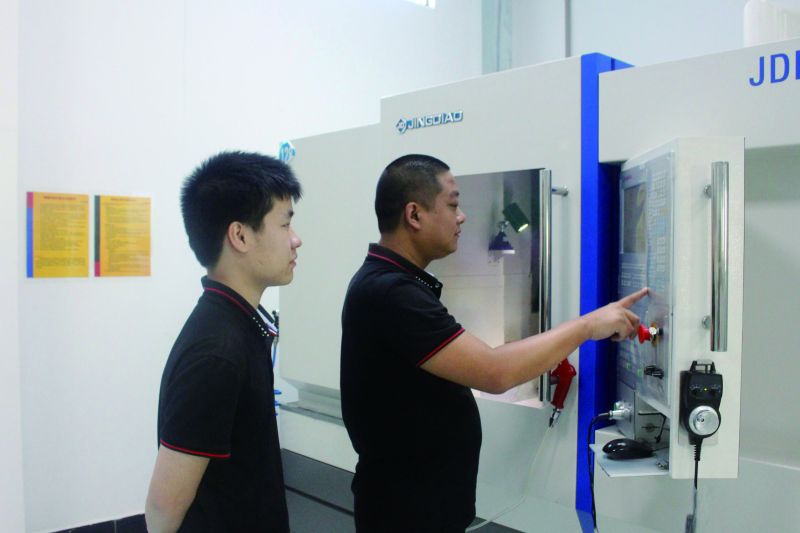
CNC & EDM machining
High-speed milling, wire EDM and sinker EDM from one plan.
Heat treatment
Hardened to the HRC on your drawing; every batch Rockwell-tested.
Grinding & coating
Finish-ground to ±0.002 mm, then PVD, nitriding or polish as specified.
Inspection & export
CMM report, rust protection, VCI wrap and crated shipment.
Machining, EDM and Metrology Under One Roof for Precision Tooling Components
Cutting, grinding and measuring all happen in our plant in Humen, Dongguan. Tolerances are never lost between subcontractors, and one team answers for the finished part.
High-speed & 5-axis machining
Hardened-steel milling for core inserts, electrodes, die plates and complex forms.
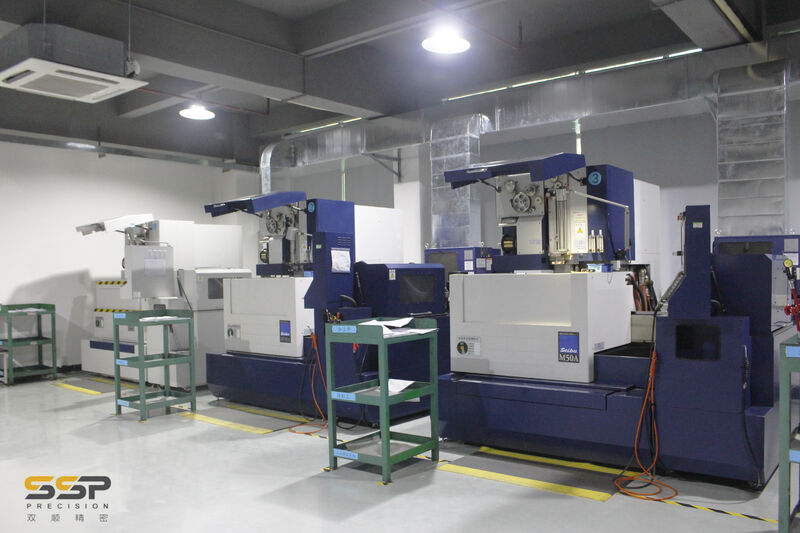
Wire EDM
Seibu and Sodick wire EDM for punch profiles, die openings and sharp internal corners.
Sinker & small-hole EDM
Ribs, blind pockets, start holes and textured surfaces in hardened steel.
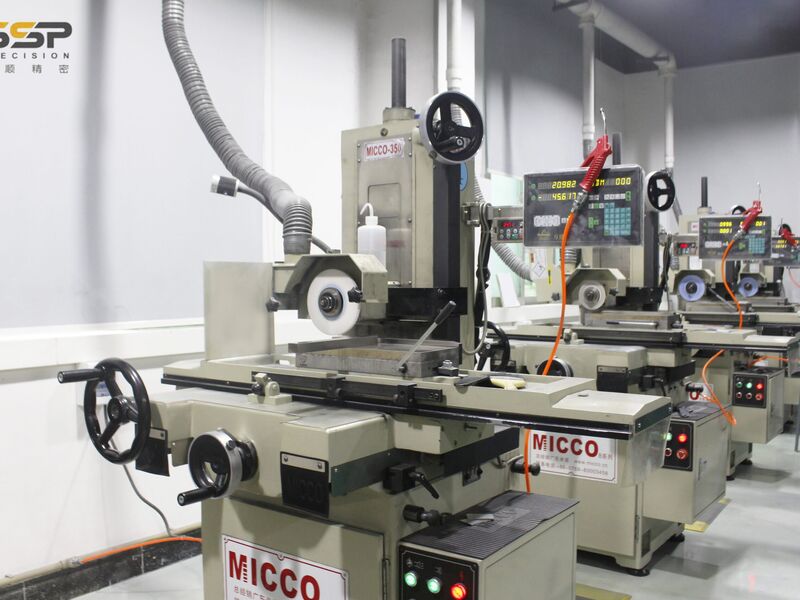
Precision grinding
Surface, profile and cylindrical grinding to ±0.002 mm on critical diameters and faces.
Metrology
CMM, optical comparator, video measuring system, height gauges and Rockwell hardness testing.
Heat treatment control
Hardening and tempering to the HRC on your drawing, verified in-house on every batch.
The full machine list is on our manufacturing capabilities page.
Custom Punches, Die Inserts and Mold Components
The wear parts and precision components that keep stamping dies and injection molds running, each built to your drawing.
Precision Punches
Round, shaped and custom punches in D2, M2/SKH51 and carbide, profile-ground to ±0.002 mm for consistent clearance over long press runs.
Die Inserts & Buttons
Hardened die inserts, carbide die buttons and replaceable segments that restore cutting edges without rebuilding the whole die.
Guide Pins, Pillars & Bushings
Ground guide pins, pillars and bushings that keep upper and lower die halves aligned, to DIN, ISO or your own dimensions.
Die Plates & Retainers
Die plates, stripper plates, shoes and punch retainers with precision-ground datum faces for repeatable reassembly.
Lifters & Pilots
Stock lifters, pilots and locating parts that keep strip feed and progression accurate in progressive dies.
Mold Core & Cavity Inserts
Core and cavity inserts, ejector pins and slides in P20, H13 and S136, mirror-polished to Ra 0.05 µm where the part needs it.
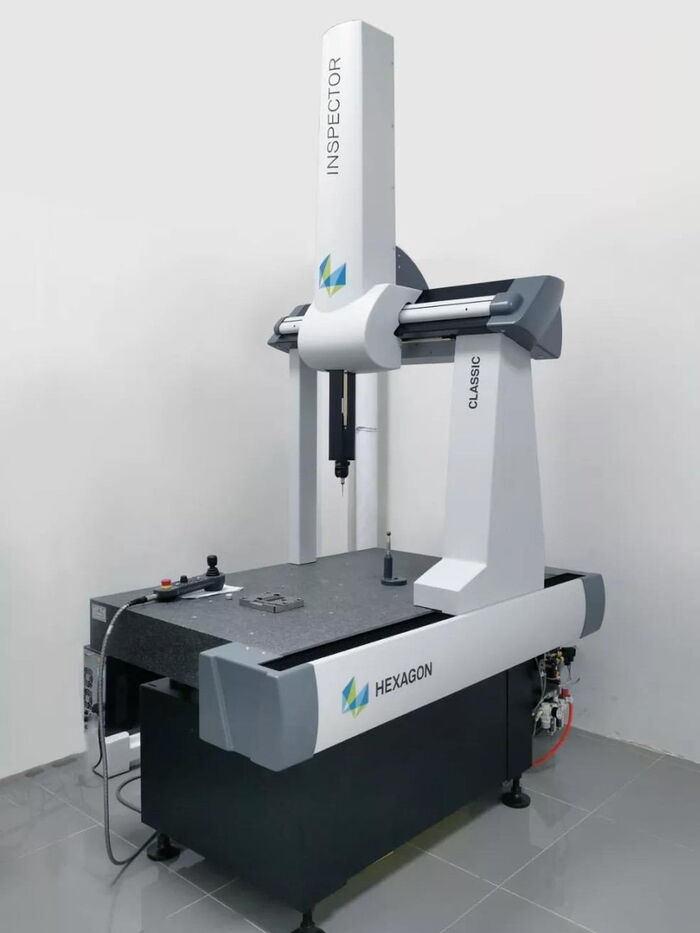
Inspection Data With Every Shipment
Parts are checked against your drawing at each stage, not only at the end. Our quality system is certified to ISO 9001:2015 and IATF 16949.
- Critical dimensions verified on CMM, with a report you can file
- Profiles and cutting edges checked on optical comparator and video measuring system
- Rockwell hardness tested on every heat-treated batch
- Surface roughness (Ra) measured on ground and polished faces
- Material certificates and traceability kept for every order
- First article inspection (FAI) and PPAP documents on request
Why Global Manufacturers Choose SSP for Tooling Spare Parts
Toolmakers who build complete dies and molds, a documented quality system, and export logistics that work for buyers in 40+ countries.
Toolmakers, not a parts broker
We design and build complete progressive dies and molds, so spare parts are made with the whole tool in mind.
Competitive landed cost
China-based production with export packing included, and EXW, FOB or DDP terms quoted up front.
Prototype to production volume
From one urgent replacement punch to repeat batches of interchangeable spares on a fixed schedule.
DFM with every quote
Engineers flag tolerance, material and heat-treatment risks before machining starts, at no extra charge.
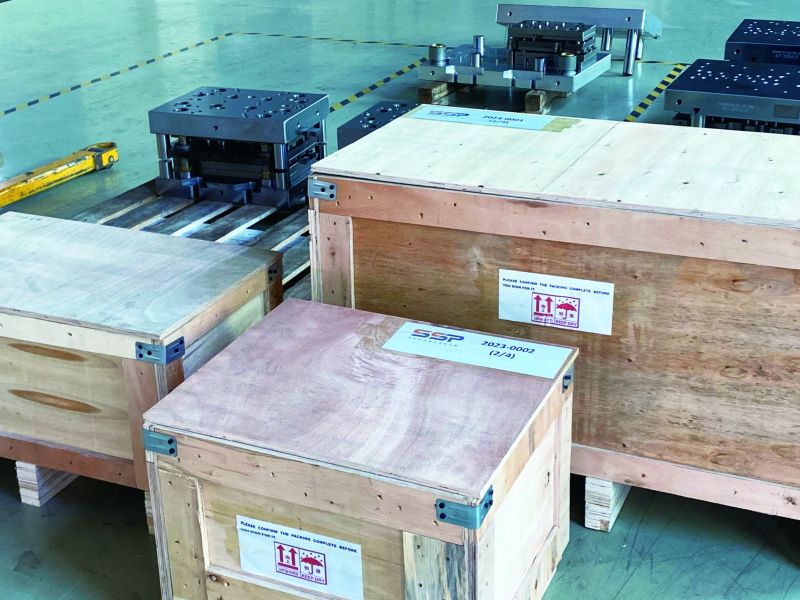
Precision Made in China. Delivered Worldwide.
Parts are rust-protected, VCI-wrapped and crated in Dongguan, with export documents and HS codes prepared for your customs broker. For planning, see our China tooling lead-time data.
- USA & Canada
- Europe & UK
- Japan & Korea
- Australia & NZ
- Southeast Asia
- Middle East
Tool Steels, Carbide and Alloys Held to ±0.002 mm
We machine and grind the grades your drawing calls for, with mill certificates on file. Choosing a steel? Our tool steel HRC hardness chart and D2 vs DC53 comparison can help.
Ground tolerance on critical diameters and profiles
Mirror polish on mold core and cavity inserts
Rockwell-tested on every heat-treated batch
Surface Treatments That Extend Tool Life
The right treatment reduces wear, galling and corrosion. Coating and finishing are specified with the part and controlled by the same project engineer.
Mirror Polishing
Ra 0.05 µm by progressive diamond polishing, for mold cavities where part appearance and clean release matter.
Hard Chrome Plating
Electrolytic hard chrome (HV 800–1000) for wear resistance on punches, pins and sliding components.
TiN / TiCN / TiAlN PVD
Physical vapor deposition coatings (HV 2,300–3,000) that raise surface hardness, cut friction and can extend punch and die life several times over uncoated steel.
Gas & Plasma Nitriding
A diffused nitrogen-rich case that improves fatigue strength and seizure resistance with minimal dimensional change.
Black Oxide
Chemical conversion coating for mild corrosion resistance and low glare on non-wear surfaces.
DLC Diamond-Like Carbon
A hard, very low-friction carbon coating (typically HV 1,500–3,000) for galling-prone forming and sliding parts.
EDM Surface Texturing
Controlled EDM textures on mold inserts for release behavior and matte part finishes.
Electroless Nickel
Uniform EN coating (HV 500–700) that covers complex geometry evenly and resists corrosion.
Complete Precision Engineering Portfolio
Beyond tooling spare parts, SSP builds complete tools and machined parts for stamping, injection molding and industrial equipment.
Stamping Die
Custom progressive, compound and transfer stamping dies with precision-ground components, hardened tool steel and in-house press tryout.
Injection Mold
Single-cavity, multi-cavity, hot runner and family injection molds in P20, H13 and S136 with mold flow analysis.
Machine Parts
CNC-machined industrial components: shafts, flanges, housings and brackets in steel, aluminum and specialty alloys.
Standard Tooling Spare Parts
Catalog punches, bushings, pilots, lifters and guide pins to DIN, ISO, HASCO and MISUMI standards.
Custom Tooling Spare Parts Manufacturing: Questions Buyers Ask
What do you need to quote a custom tooling spare part?
Send a 2D drawing or 3D model, drawing revision, quantity, material, hardness and coating requirements. For tooling spare parts manufacturing, identify the datums, critical fits, cutting edges and dimensions requiring a report. Include a photograph of the assembly if the component's function is unclear. Tell us whether the enquiry is for one urgent replacement or repeat batches of interchangeable spares. State the required delivery date and inspection documents. Use our quotation checklist to assemble the information before review.
Can you make a spare part without a drawing?
SSP can review a worn or broken component, measure accessible features and prepare a replacement drawing for approval. For tooling spare parts manufacturing from a sample, distinguish wear from the original geometry: a damaged cutting edge or worn guide diameter may not represent the intended size. Supply mating-part dimensions, an old drawing or a new spare if available. Agree datums, fits, material, hardness and the inspection scope before machining. Approve the reconstructed drawing and identify any dimensions that require fitting during installation.
Is there a minimum order quantity?
SSP's stated spare-parts service accepts single replacements as well as batches. Quote tooling spare parts manufacturing against the component, quantity and delivery requirement, because setup, heat treatment, finishing and inspection can affect the economics of a small order. For repeat supply, specify the approved drawing revision, material and acceptance criteria consistently. Tell us whether future orders need to interchange without additional fitting. Agree how drawing changes are approved and whether samples must be checked before a larger batch is released.
How long does it take to make tooling spare parts?
The page lists an indicative lead time of 7–15 days for tooling spare parts manufacturing, depending on complexity, heat treatment and finishing. Request a confirmed schedule for the actual component. Identify whether the requested date means dispatch from Dongguan or arrival at your factory, and allow for transport and customs. Clarify approval dates for reconstructed drawings, material substitutions or sample parts. For an urgent spare, send the drawing and complete requirements together so the engineering team can evaluate the feasible process and timing.
What tolerance can you hold on punches and inserts?
This page lists ±0.002 mm grinding capability on selected critical diameters and profiles. For tooling spare parts manufacturing, agree which features require that tolerance and which can use the drawing's general tolerance. Define measurement datums, surface finish, mating clearances and inspection methods before manufacture. Check whether the final size is specified before or after coating. A precise standalone measurement does not by itself establish fit in a worn assembly. Where appropriate, supply the mating part or its dimensions and agree installation or trial responsibilities.
What documents come with the parts?
Agree the inspection pack for tooling spare parts manufacturing before placing the order. Specify the drawing revision, critical dimensions, material identification, hardness requirements and finish or coating records. This page lists dimensional reports, material certificates and hardness results, with FAI and PPAP documents available on request. Confirm the requested format, sampling quantity and document scope in the quotation. Identify any customer-specific acceptance criteria or independent testing. Keep the approved drawing and report together so replacement batches can be checked against the same requirements.
Do you make parts to DIN, ISO, HASCO or MISUMI standards?
SSP lists standard-dimension items in its tooling spare parts catalog and reviews modified or fully custom components to your drawing. For tooling spare parts manufacturing, a standard or supplier name alone may not identify every dimension, material or finish. Send the part number, referenced edition or drawing and any required modifications. Compare installation dimensions, critical fits and tolerances with the existing assembly. Agree whether the quoted item is a standard component, an equivalent made-to-print part or a custom replacement before ordering.
How are spare parts packed and shipped?
Specify the destination, delivery term and packing requirements with the tooling spare parts manufacturing enquiry. This page lists corrosion protection, VCI wrapping and boxed or crated shipment, with courier, air and sea options. Identify precision edges, polished surfaces or matched sets that need individual protection and labeling. Confirm whether quoted EXW, FOB or DDP terms include the services you need, and coordinate customs information with the receiving team. Record the quantity and drawing revision on the packing documents so maintenance staff can identify each replacement correctly.
Request a Quote for Custom Tooling Spare Parts
Upload your drawings or photos of the worn part below. A project engineer replies within 24 hours with pricing, lead time and DFM notes.
- No minimum order
- ±0.002 mm ground tolerance
- ISO 9001:2015 · IATF 16949
- Ships to 40+ countries
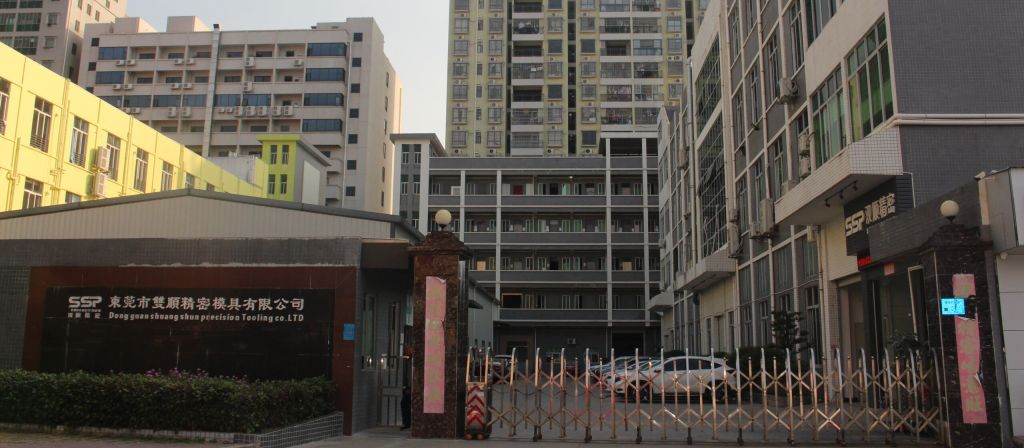
SSP · Custom tooling spare parts manufacturer · Humen, Dongguan, China · Engineers reply Mon–Fri, 9:00–17:00 China Standard Time